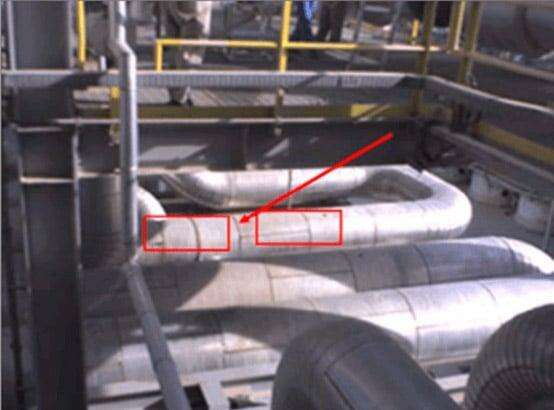
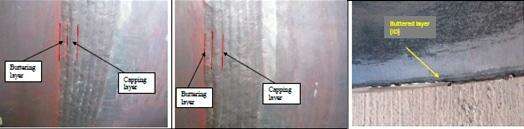
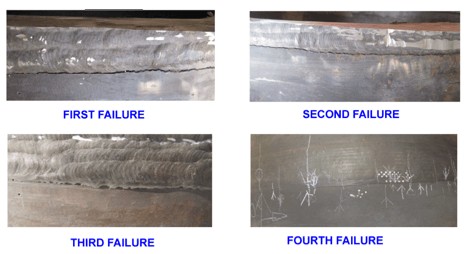
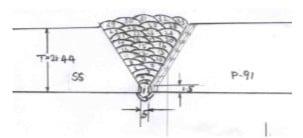
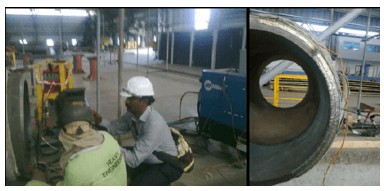
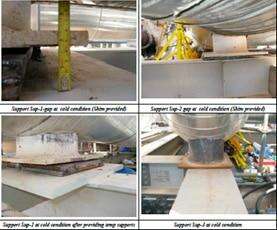
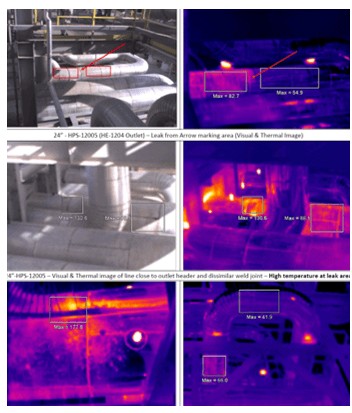
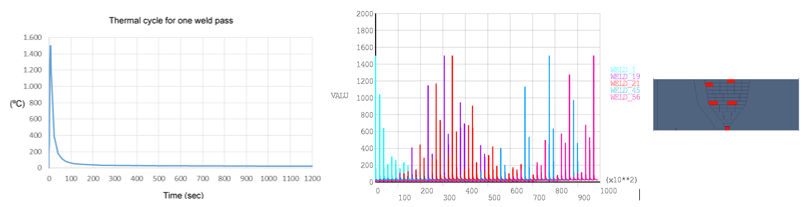
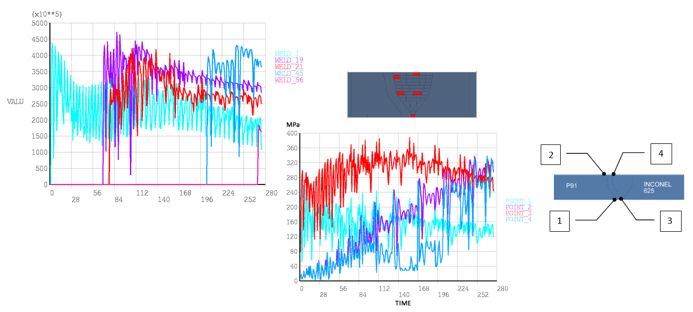
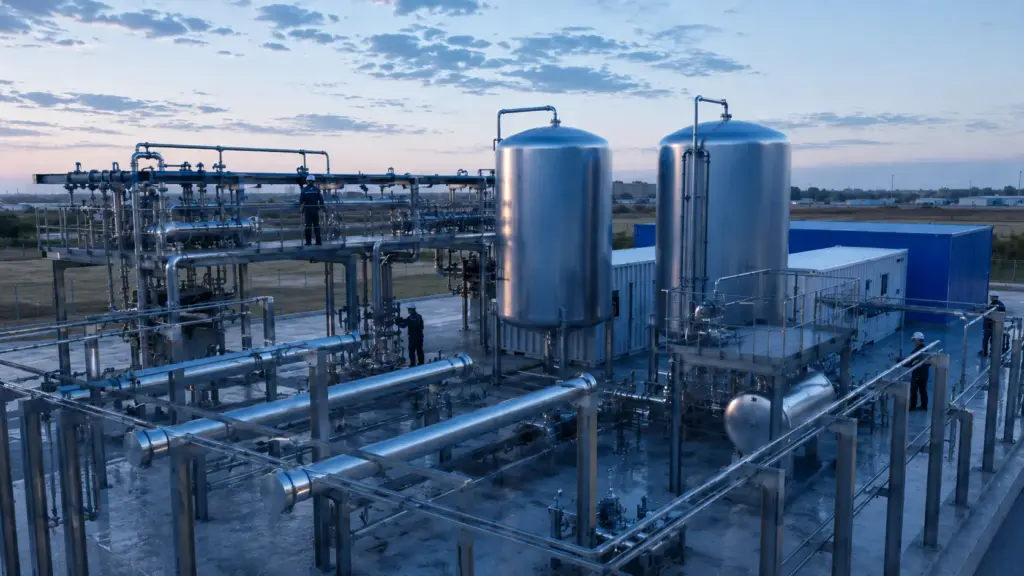
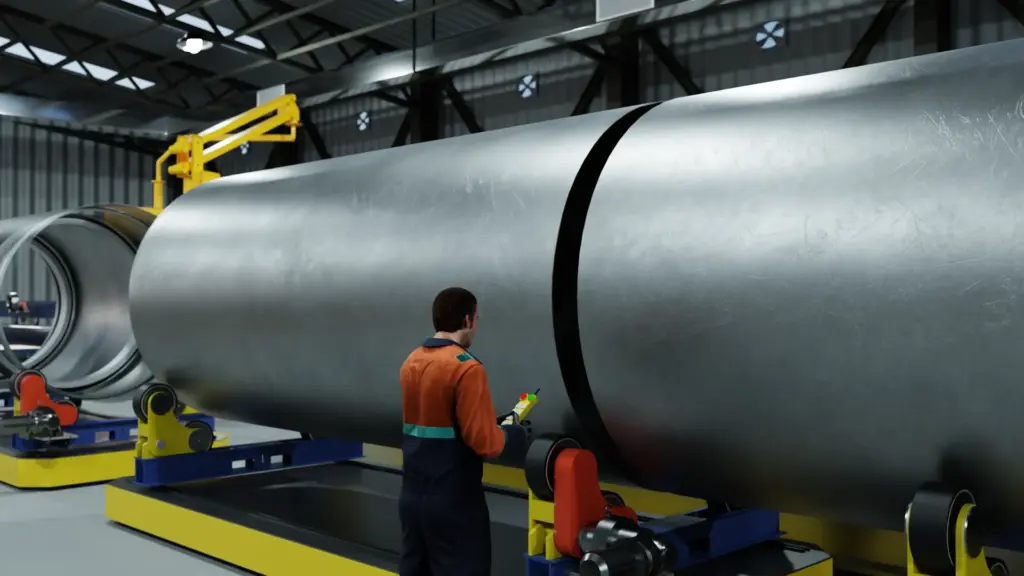
Fig. 1: 24″ High pressure steam pipe actual disposition and welding features
Design and Fabrication Data:
Operation Data
Regular Operation
Best Mechanical and Process Engineering Practices
2.1: DETAIL LEVEL 1
2.2: DETAIL LEVEL 2
2.3. DETAIL LEVEL 3
Observations and Evidence
Root Cause Analysis and Determination of Failure Cause
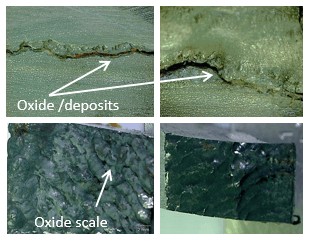
✔ Sreroscopy ⇒ oxide deposits ⇒ CAPING PASS
✔ Fractography ⇒oxide fragments on internal and external surfaces
✔ Chemical composition ⇒acording to materials specifications requirements
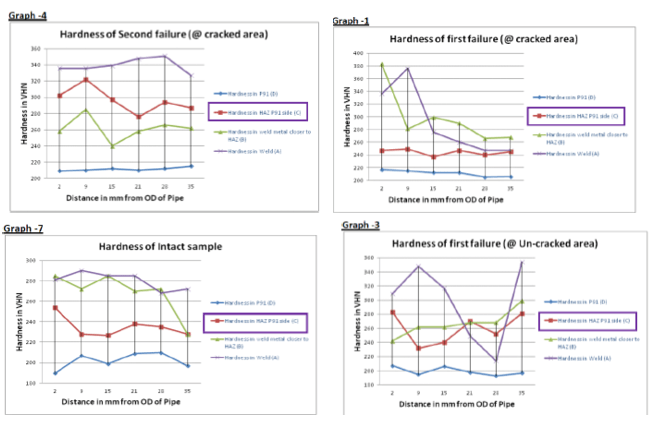
✔ Identification of high hardness points in HAZ areas of P91 and INCONEL, coincident with the location of cracks
✔ Warm-up 200ºC
✔ Welding GTAW
✔ Welding 5g Weld / 2G buttering
✔ PWHT in buttering ⇒ no PWHT in welding
✔ Support Systems and stress Calculation with no anomalies detected
✔ Insulation temperatures are higher in leakages area
✔ Optimal PWHT treatment on weld area is defined
⇒ Decreasing residual stresses, decreasing material hardness, improving toughness
✔ Spacial care with reached temperatures (do not exceed 760ºC)
⇒ Fragilization issues
✔ Verification of residual stresses by means of FEA, and physical tests
Describe your case and a CADE specialist will review it.