Contactar

Root Cause Analysis And Corrective Measures Of Dissimilar Weld Joint Failure In A High Pressure Steam Pipe

Problem definition

  • During the operation of a petrochemical plant (located in Middle East), recurring appearance of cracks in dissimilar metal welding joint of a critic, high pressure steam pipe has been detected (2010-2014).
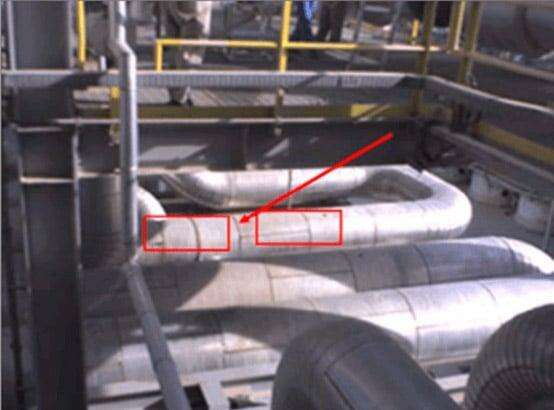
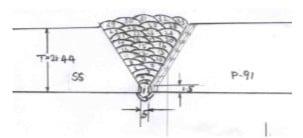
  • Cracks appear periodically over the same area, which is the butt weld joining two pieces made of different materials A-335-P91 and SS347H. Weld material is INCONEL625.
  • 24” diameter and great thickness due to severe operating conditions: tª=530ºc, p=110 bar
  • None of the reparations conducted so far has been effective to stop recurring breakage after 6-12 months.

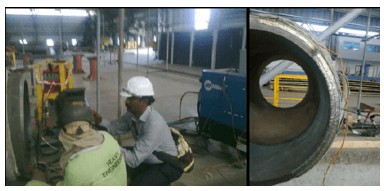
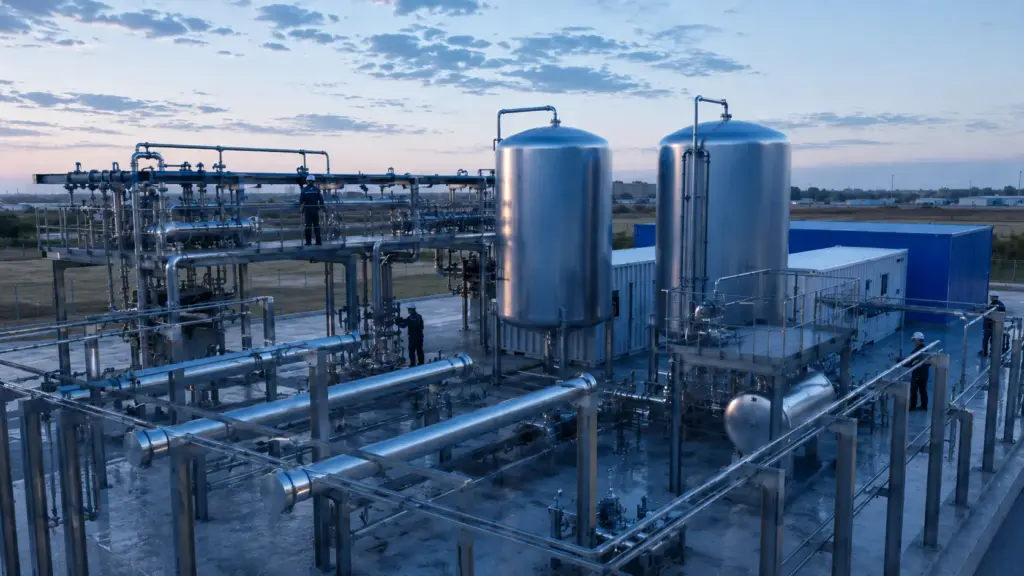
Fig. 1: 24″ High pressure steam pipe actual disposition and welding features

Methodology

Design and Fabrication Data:

  • Welding detail
  • Welding process
  • Pre and Post welding thermal treatments
  • Materials (properties, storage…)
  • Inspections and NDT

Operation Data

  • Previous observations and Evidences
  • Failures record and details (critical area pictures, crack pictures…)
  • Macrographs, metallography, hardness tests, traction tests, chemical composition.
01

Regular Operation

  • Pipe and welding on operation conditions
  • Welding process
  • Residual stresses
02

Best Mechanical and Process Engineering Practices

  • Simulation: FEA
  • International Codes (ASME, FFS)
  • Physical Modelling (understanding how it works)
  • Tests and Hypothesis Modelling
  • Corrective Measures Modelling

2.1: DETAIL LEVEL 1

  • Piping and welding analysis under operation conditions

2.2: DETAIL LEVEL 2

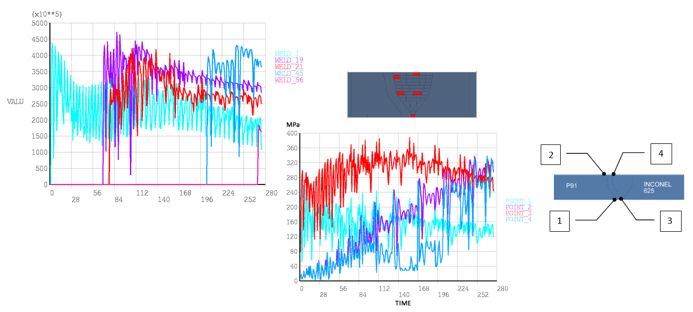
  • Welding process simulation

2.3. DETAIL LEVEL 3

  • Tests to obtaining residual stresses
03

Observations and Evidence

  • Laboratory Tests
04

Root Cause Analysis and Determination of Failure Cause

  • Specific proposal of corrective measures
  • Modification of welding detail + Pipe spool
  • PWH
  • Modification of welding process and pass sequences
  • Modification of welding filler material

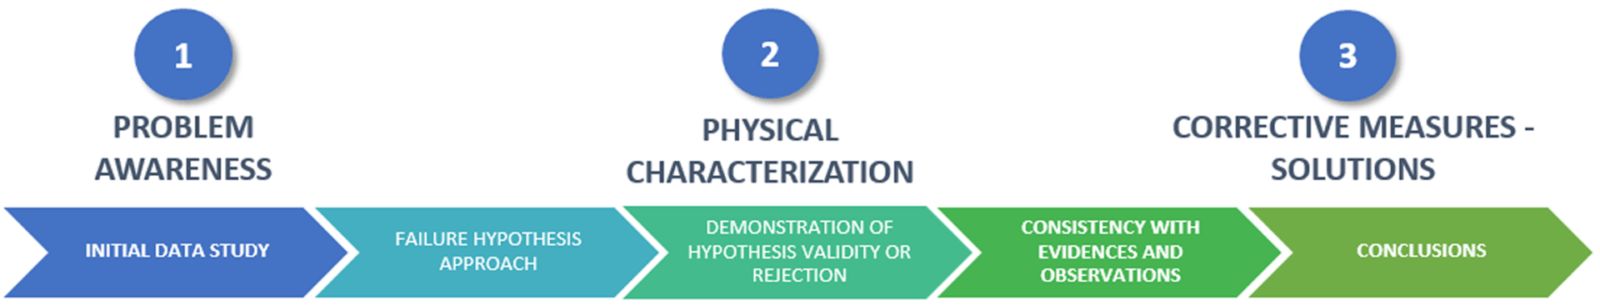
1. Problem Awareness

1.1 Failure identification

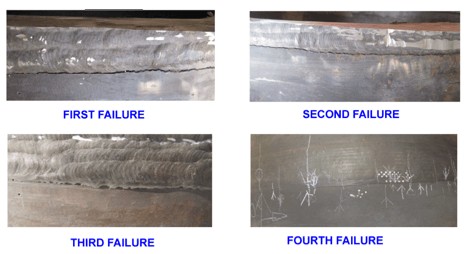
⇒ FAILING EVERY 6-12 MONTHS

1.2 Location and Size Craks

  • CIRCUMF. between 100º-270º
  • LENGTH. 250mm-400mm
  • Crack on melting area
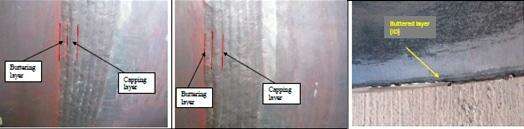
  • buttering Inconel 625 – P91

1.3 Inspections and NDT

✔ Full cracks VT and superficial cracks (PT-NDE)
✔ Internal part of the pipe in crack location ⇒ inadequate filling

1.4 Fractography, Steroscopic Examination and Chemical Composition

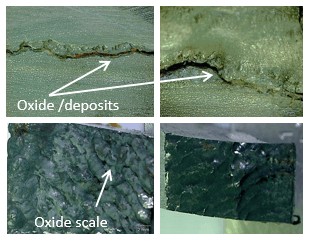
✔ Sreroscopy ⇒ oxide deposits ⇒ CAPING PASS
✔ Fractography ⇒oxide fragments on internal and external surfaces
✔ Chemical composition ⇒acording to materials specifications requirements

1.5 Metalography

✔ Tempered martensite structure in P91, HAZ
✔ Dendritic austenitic structure in INCONEL and Buttering
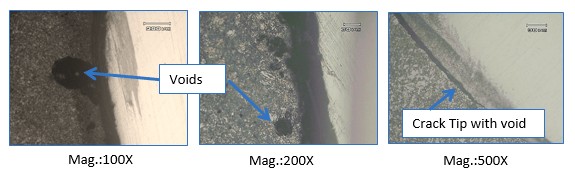
✔ Tempered martensitic structure with ferrite in crack location area
✔ Presence of nucleation of voids and spheroidal graphite

1.6 Hardness test

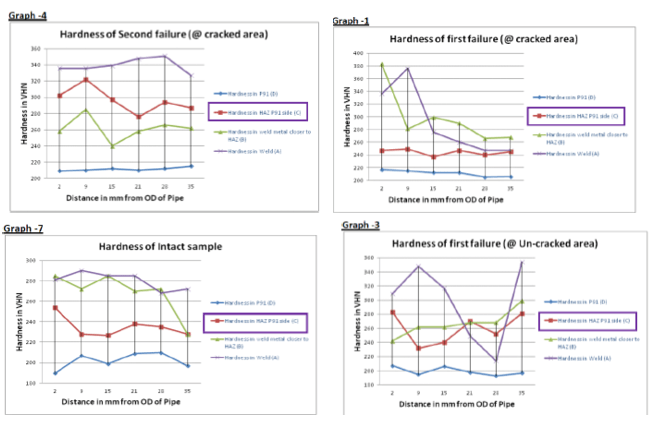
✔ Identification of high hardness points in HAZ areas of P91 and INCONEL, coincident with the location of cracks

1.7 Welding process and heating treatments

✔ Warm-up 200ºC
✔ Welding GTAW
✔ Welding 5g Weld / 2G buttering
✔ PWHT in buttering ⇒ no PWHT in welding

1.8 Operation conditions And support systems

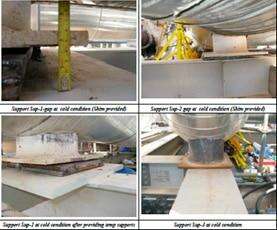
✔ Support Systems and stress Calculation with no anomalies detected
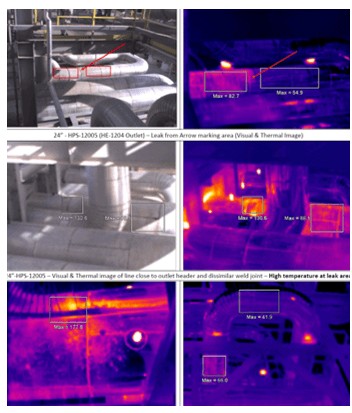
✔ Insulation temperatures are higher in leakages area

2. Physical characterization

2.1 Detail Level 1- Pipe & Weld Analysis under Operation Conditions

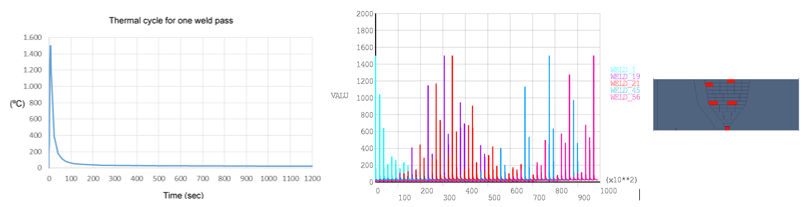
2.2 Detail Level 2- Welding Process Simulation

2.3 High Pressure Steam Pipe Failure Causes

Solution: Corrective Measures

Installation of Spool Pipe section between P91 and SS347H

Definition of new PWHT

✔ Optimal PWHT treatment on weld area is defined
⇒ Decreasing residual stresses, decreasing material hardness, improving toughness
✔ Spacial care with reached temperatures (do not exceed 760ºC)
⇒ Fragilization issues
✔ Verification of residual stresses by means of FEA, and physical tests
Modification of Welding Pass Sequence

About the project

  • Solution proposed has solved a critical and recurring problem which involved a high cost in terms of plant availability.
  • Root cause analysis and project execution was subjected to hard constraints of time, and had to be solved over a 2-months period (remaining time until Turnaround).
  • Solid and consistent methodology thanks to simulation.
Do you have a similar project?

Describe your case and a CADE specialist will review it.

Other projects